An abrasive slurry pump for mineral processing plant duty should be selected around the slurry, the operating point, and the maintenance reality of the circuit, not simply by pipe size or a quoted flow rate. A pump that looks adequate on paper can fail early when coarse particles, fluctuating solids, corrosive water chemistry, or an unstable feed condition are overlooked.
The most suitable pump is usually the one that delivers the required flow and head while operating near its efficient range, keeps wear manageable, and can be maintained without creating excessive downtime. That requires looking beyond the pump curve. The size, hardness, concentration, and shape of solids often matter as much as the liquid volume being moved.
Start with the slurry, not the pump model
Mineral processing slurries vary widely between crushing, grinding, classification, flotation, thickening, tailings, and concentrate handling. Calling all of them “abrasive” is not enough for pump selection. A fine grinding-circuit slurry behaves differently from a tailings stream containing coarse, angular particles, even if both have a similar solids concentration.
Before comparing pumps, define the operating slurry as clearly as possible:
- Particle size distribution: The largest particles influence passage size and blockage risk, while the full distribution affects wear behavior.
- Particle hardness and shape: Hard, sharp particles generally cause more aggressive cutting wear than rounded or softer particles.
- Solids concentration: Higher concentration changes slurry density, increases the power demand, and may affect how readily solids remain suspended.
- Specific gravity: Both the mineral and the slurry specific gravity affect head, power, and pump sizing.
- Corrosive conditions: Acidity, alkalinity, dissolved chemicals, chloride content, and process reagents can change the preferred wetted material.
- Temperature and feed variation: A pump designed for a stable average condition may struggle when density, flow, or particle size changes during normal operation.
A common purchasing error is to specify the pump from the average slurry condition alone. In a plant, the difficult condition is often more relevant: a cyclone feed stream at a higher-than-normal density, a sump that sees intermittent coarse material, or tailings that thicken as a downstream unit changes operating conditions. The selected pump needs enough margin for credible variation, but not so much oversizing that it runs inefficiently or causes unnecessary recirculation.
Match flow and head to the real system curve
Flow and head are essential, but they should be calculated from the complete piping system rather than estimated from nominal pipe diameter. Static lift, pipe length, bends, valves, hose sections, elevation changes, and slurry friction all contribute to the required head. Slurry friction can be substantially different from clear-water friction, particularly when the solids are coarse or the line velocity is poorly chosen.
The pump curve should be reviewed at the actual slurry duty. A centrifugal slurry pump does not deliver the same head and efficiency with a dense slurry as it does with water. Suppliers may apply correction methods for slurry behavior, but the important decision is practical: confirm that the required duty point remains within the pump's recommended operating region after accounting for the material being pumped.
Operating too far left on the curve can create recirculation, vibration, heat, and uneven wear. Operating too far right may reduce available head, raise power demand, and increase velocity-related wear. The best point is rarely the maximum flow shown on a curve. It is the point where the pump can tolerate expected process changes without repeatedly moving into an unfavorable operating zone.
Do not treat line velocity as a simple “higher is safer” rule
The pipeline needs enough velocity to keep solids from settling, especially in horizontal runs, low points, and intermittent service. However, excessive velocity accelerates wear in pipes, elbows, valves, and the pump itself. It can also increase power consumption. The appropriate range depends on particle characteristics, concentration, pipe geometry, and whether the system runs continuously.
This is why pump and pipeline decisions should be made together. Reducing a pipe diameter to increase velocity may solve a settling concern but create high friction losses and rapid wear. Increasing pipe diameter may reduce friction but permit solids to settle if flow drops. The pump choice must support the intended transport regime across normal operating conditions, including start-up and turndown where relevant.
Choose materials for the wear mechanism
There is no universally best material for abrasive slurry service. The right choice depends on whether the dominant problem is abrasion, corrosion, or a combination of both.
Hard-metal components are often appropriate for abrasive mineral slurries, but they are not automatically suitable for every duty. Large tramp material, severe impact, or a corrosive chemistry can change the decision. Elastomer-lined pumps can provide good performance with fine, non-sharp particles in compatible chemical conditions, but they are generally less suitable where large, sharp solids or high-impact service can damage the liner.
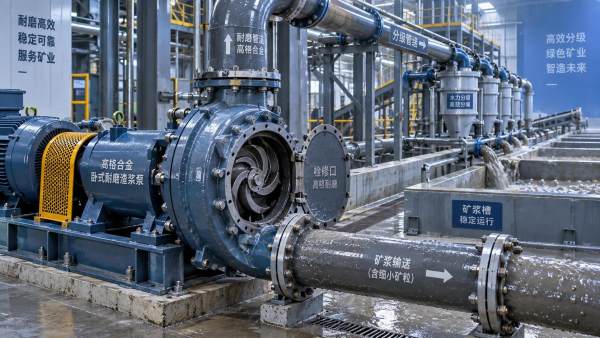
The casing, impeller, throatbush, frame plate liner, and other wetted parts should be considered as a wear system. Replacing only the impeller material while ignoring the rest of the wet end may not improve total service life. Wear also affects hydraulic performance: as clearances increase, recirculation rises and the pump may no longer meet its duty before a component visibly fails.
Passage size and impeller design determine whether the pump keeps running
Abrasive wear is costly, but blockage and unstable operation can be even more disruptive. The pump needs sufficient internal passage size for the expected particle size and any credible oversize material. This is especially important in mill discharge, coarse tailings, dewatering sumps, and transfer duties downstream of crushing or screening equipment.
Impeller design is part of that decision. Closed impellers can offer strong hydraulic performance in controlled fine-slurry duties, while more open designs may provide greater tolerance for solids passage and allow some wear adjustment. The correct arrangement depends on the application; an impeller selected only for peak efficiency may be less forgiving when the feed becomes coarser or the sump receives debris.
Look at the complete flow path, not just the impeller inlet. Restrictions can occur at the suction liner, throatbush, volute entrance, discharge connection, and valves. A nominally large discharge flange does not guarantee a clear solids passage through the whole pump.
Protect suction conditions and avoid cavitation
Slurry pumps are often installed below sump level because flooded suction is more forgiving. Even then, poor suction design can shorten pump life. Long suction lines, restrictive fittings, air ingress, vortexing, poor sump geometry, and insufficient liquid level can reduce the pressure available at the impeller inlet.
Cavitation is not just a noise issue. It can erode components, create vibration, reduce flow, and complicate diagnosis because its symptoms can resemble ordinary wear or mechanical problems. In abrasive service, cavitation damage and particle erosion can act together.
A well-designed installation gives attention to suction pipe routing, air management, sump level control, and the pump's required suction conditions. If a pump is fed from an agitated tank or sump, consider whether entrained air, froth, or variable submergence will occur. A pump suitable for dense slurry may still perform poorly if its inlet receives an unstable, aerated feed.
Mechanical design matters when maintenance windows are short
Wet-end materials receive most of the attention, but the mechanical end determines whether the pump can carry the required load reliably. Check the bearing assembly, shaft stiffness, seal arrangement, lubrication method, drive configuration, and baseplate design against the actual duty. A large pulley drive, high-density slurry, frequent starts, or variable-speed operation may place different loads on the assembly than a simple water-pumping application.
Seal selection deserves a separate review. Some slurry pumps use expeller or dynamic sealing arrangements where operating conditions permit; others require packing, mechanical seals, or auxiliary flush arrangements. There is no seal choice that is automatically best. The practical question is whether the seal system matches the pressure, solids level, downtime tolerance, available seal water, and environmental requirements of that location.
Maintenance access is also a selection criterion. In a crowded concentrator, a pump that requires major pipework removal for routine wet-end work creates costs that do not appear in the initial purchase price. Consider lifting access, component weight, cartridge or back-pull-out arrangements where available, spare-part interchangeability, and whether technicians can safely inspect wear components without extensive disassembly.
Evaluate total operating cost, not only the purchase price
The least expensive pump at installation can become the costly choice if it consumes excess power, requires frequent unplanned shutdowns, or needs difficult-to-source parts. At the same time, selecting the largest or most heavily built pump without a defined operating need can add capital cost and make the system harder to control.
For an abrasive slurry pump for mineral processing plant service, evaluate the likely cost drivers together:
- Expected wet-end wear life under the intended slurry conditions
- Power demand at the normal and high-density operating points
- Labor and downtime required for inspection and component replacement
- Availability of compatible wear parts, bearings, seals, and liners
- Consequences of a pump outage for upstream and downstream plant production
- Ability to adjust for wear, process changes, or future capacity changes
Wear life should not be treated as a fixed promise. It depends heavily on the material being processed and how the plant operates. A supplier can provide a useful starting recommendation, but the final selection is stronger when it is based on representative slurry information and a realistic duty profile.
Information to prepare before requesting a pump selection
A detailed request makes it easier to compare proposals fairly and prevents suppliers from sizing around assumptions that do not match the plant. Prepare a duty sheet covering required flow range, total dynamic head, pipe layout, slurry density, solids concentration, particle size distribution, mineral hardness, liquid chemistry, temperature, operating hours, and installation arrangement.
Include the expected abnormal conditions, not only the design target. State whether the pump must handle start-up surges, occasional coarse particles, variable sump levels, intermittent operation, or changes in ore type. Also identify whether the service is critical to production or has standby capacity. A duty with a parallel standby pump may prioritize maintainability and quick changeover differently from a single pump that stops the entire circuit.
The goal is not to find a pump with the hardest materials or the largest motor. It is to select a balanced pumping system that keeps solids moving, resists the actual wear mechanism, operates in a stable range, and can be serviced within the plant's maintenance constraints. That is the standard against which an abrasive slurry pump should be judged.
 Sep 22, 2026How Does an OEM Slurry Pump Custom Order Process Work?Delin OEM slurry pump custom order process: learn how duty analysis, material selection, seal options, testing, and commissioning create reliable pumps for demanding slurry applications.
- Sep 23, 2026Which Pump Is Suitable for High-Concentration Tailings Disposal?High concentration slurry pump for tailings disposal: learn how to select a heavy-duty centrifugal pump with wear-resistant materials, reliable sealing, and pipeline-matched performance.
- Sep 22, 2026How to Choose a Corrosion-Resistant Pump for Acid Mine DrainageCorrosion resistant pump for acid mine drainage: learn how to match materials, seals, hydraulics, and solids handling for longer service life.
- Sep 23, 2026What Should a Mineral Processing Plant Look for in an Abrasive Slurry Pump?Abrasive slurry pump for mineral processing plant selection: compare slurry properties, pump curves, wear materials, suction design, and maintenance factors for reliable performance.
Get a Quote
Please leave your information and email address, and we will contact you as soon as possible.