Froth Pump vs. Standard Slurry Pump: What's the Difference?
A froth pump is designed to move abrasive slurry containing substantial entrained air, while a standard slurry pump is primarily designed for mixtures with limited air content. Both must resist wear from solids, but a froth pump also needs to admit and handle an unstable mixture that can interfere with impeller filling. Choosing a standard slurry pump solely because its liquid-slurry duty point looks suitable can lead to surging, reduced throughput, and air accumulation at the inlet.
The distinction is most important when flotation concentrate or another frothy stream enters the pump directly. Where air has time to separate before the pump, a standard slurry pump may be suitable. The choice depends on the condition of the slurry at the pump inlet, not simply on whether the upstream process produces froth.
What Changes When Air Enters the Slurry?
A centrifugal slurry pump transfers energy from its rotating impeller to the mixture. With relatively little air present, the pump can generally be evaluated using liquid flow, solids properties, and the required discharge head. Entrained air complicates that picture: bubbles change the mixture density and compressibility, and air can collect near the impeller eye instead of moving steadily through the pump.
When air accumulates at the inlet, the impeller may receive less liquid and solids than expected. The discharge can fluctuate, the pump may lose prime, and the motor load may become unstable. These symptoms are especially troublesome when the froth varies over time, because a pump that runs acceptably during a low-air period can struggle when the incoming froth becomes more voluminous or persistent.
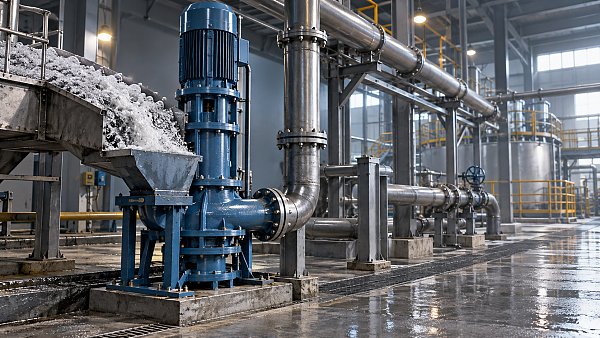
Froth pumps address this problem through designs intended to improve the entry and handling of aerated slurry. Depending on the pump design, these features can include a larger inlet, an inducer or specialized impeller geometry, and a feed arrangement that promotes the separation or movement of air. A vertical froth pump may use a tank designed to receive froth and direct slurry toward the pump inlet. Horizontal froth-duty pumps use different arrangements, so the label alone does not establish how a particular pump manages air.
Both categories include different configurations and material options. A froth-capable inlet does not automatically make a pump suitable for every abrasive or corrosive slurry, and a standard slurry pump is not necessarily unsuitable merely because occasional bubbles are visible.
Compare the Feed at the Pump Inlet
Start with the actual feed condition. A flotation cell may produce a deep, stable froth that travels directly into a pump tank. In that arrangement, the pump must handle the froth as delivered. If the same stream passes through a well-designed separation or collection stage first, some air may escape before the slurry reaches the inlet. The second arrangement can present a much less demanding air-handling duty, even though the material came from the same process.
Observe more than the appearance of the froth surface. Large visible bubbles can collapse quickly, while finer bubbles may remain dispersed within the slurry. Frother chemistry, solids characteristics, agitation, and residence time all affect how readily air separates. A quiet-looking feed tank is therefore not proof that the slurry entering the suction contains little air.
Feed variation also matters. Record conditions during normal production, startup, and changes in flotation performance. Note whether the tank level rises while discharge falls, whether flow oscillates, and whether the pump repeatedly loses prime. These observations help distinguish a persistent froth-handling limitation from a problem that occurs only during an unusual operating state.
Use froth factor carefully
Froth factor is often used in pump selection to account for the extra difficulty of handling aerated slurry. It is not a universal correction that can be applied to any published pump curve. Definitions and selection methods vary, and a factor based only on visual appearance may miss changes in air content or froth stability.
Provide the pump vendor with the actual process description and the basis for the selected factor. Identify whether the stated flow is the liquid-and-solids slurry flow or the apparent volume of aerated froth, and identify where it was measured. Applying a froth allowance to a flow figure that already includes entrained air can distort the selection; ignoring air altogether can produce the opposite error.
Capacity and Head Do Not Tell the Whole Story
A pump curve for water or conventional slurry is a starting point, not a guarantee of froth performance. Entrained air can alter the relationship between speed, flow, and developed head. A larger standard pump selected from a conventional curve may still have difficulty admitting froth, even if its nominal capacity exceeds the calculated slurry flow.
Prepare the duty point using the required delivered slurry flow and total dynamic head. The head calculation should include the elevation difference, friction losses in the discharge line, and any required pressure at the destination. Then review that duty alongside the expected aeration, rather than folding every uncertainty into a larger flow number.
Solids concentration needs the same care. State whether concentration is expressed by mass or by volume, and include solids specific gravity. Particle size distribution and particle shape influence settling, wear, and hydraulic losses. A stream with coarse, angular particles presents a different wear duty from a fine concentrate even when both have the same reported solids concentration.
Density readings can also mislead when air is present. An instrument reading the bulk aerated mixture may indicate a lower apparent density than a measurement taken after air separation. Before using a density value to size the pump or calculate solids concentration, establish where and how it was measured.
Installation Can Decide Whether Either Pump Works
A froth pump still needs a suitable feed arrangement. Long or restrictive suction piping, abrupt changes in direction, high points where air collects, and uncontrolled feed entry can all make filling less reliable. Follow the selected pump's inlet requirements and keep the feed path as direct as the layout permits. For a vertical tank-mounted configuration, tank geometry and the way froth enters the tank form part of the pumping arrangement.
Submergence and feed level matter, but raising the tank level is not a universal cure. More liquid above the inlet can improve inlet conditions in some arrangements, while an excessively high level can cause overflow or alter upstream operation. Use the pump's specified operating range and investigate why the level is changing before adjusting it.
On the discharge side, provide enough velocity to transport the solids without allowing them to settle, while avoiding unnecessarily high velocities that increase friction and wear. The suitable range depends on the slurry and pipe layout. A control change that reduces flow to stabilize a frothy inlet can create a separate deposition problem in the discharge line.
Allow for access to liners, impellers, seals, and any adjustable wear components. Air handling does not eliminate abrasion: repeated operation at an unstable duty can complicate wear diagnosis, while worn components can further reduce performance.
Separate Air Problems From Similar Faults
Surging and low flow are evidence of an unstable system, not proof that the wrong pump type was installed. A restricted suction, insufficient feed, an air leak, a blocked discharge line, or a badly worn impeller can produce overlapping symptoms. The timing of the problem provides useful evidence.
- Flow falls as froth builds: compare tank level, feed appearance, and pump load. A rising level with falling discharge points toward an inlet or air-handling limitation, although a discharge restriction should also be ruled out.
- Performance deteriorates gradually: inspect wear clearances and internal components as well as changes in the slurry. Wear can reduce head without a corresponding change in froth.
- The pump loses prime after maintenance: examine suction joints, seals, and priming arrangements. Air drawn through a leak is a different problem from air already entrained in the feed.
- Noise or vibration appears at a particular duty: review inlet conditions and the operating point. Cavitation, air entrainment, mechanical faults, and flow instability can sound similar; noise alone does not identify the cause.
Use trend data where available: feed and discharge flow, tank level, motor current, pressure, and speed are more informative together than any one reading. Take observations under comparable production conditions, since a change in upstream air addition or reagent dosage can alter froth behavior without any change to the pump.
Making the Selection
Choose a froth-duty design when the pump must consistently receive aerated slurry and the air cannot be adequately removed before the inlet. Specify the expected range of froth conditions, not just a single average. Include the slurry flow and head, solids properties, chemistry, temperature, feed arrangement, and any known changes between startup and steady production.
A standard slurry pump is a reasonable option when the feed reaches it with limited entrained air and a stable supply, provided the hydraulic duty and wear materials match the service. If the air condition is uncertain, establish it through representative sampling, operating observations, or a suitability assessment with the pump vendor before treating a conventional pump curve as the final selection basis.
When replacing an existing pump, preserve evidence of the original problem: operating trends, wear patterns, line configuration, and the conditions under which capacity was lost. That information is often more useful than specifying the replacement from the old nameplate alone.
Related Information
 Nov 08, 2026
Why Is My Slurry Pump's Rubber Liner Peeling?
Can sharp particles make your slurry pump's rubber liner peel? Discover the warning signs, other common causes, and practical ways to prevent repeat failures.- Nov 08, 2026
Do High-Chrome Pump Parts Resist Coarse, Sharp Particles?
Will high chrome pump parts resist wear from coarse, sharp particles? Discover when they perform best and how to choose the right alloy for your slurry. - Nov 07, 2026
What Factors Affect FGD Pump Lifecycle Cost?
FGD pump lifecycle cost goes beyond purchase price. Explore how energy, slurry wear, maintenance, spares, and downtime affect your total investment. - Nov 07, 2026
Froth Pump vs. Standard Slurry Pump: What's the Difference?
Froth pump vs standard slurry pump: compare air handling, performance, and selection factors to choose the right pump for your application.

{item.title}
Get a Quote
Please leave your information and email address, and we will contact you as soon as possible.