How Do You Troubleshoot Excessive Vibration in a Slurry Pump?
To troubleshoot excessive vibration in a slurry pump, first establish whether the machine can safely continue running, then determine whether the vibration follows changes in the process or persists under stable conditions. A pump that shakes when sump level falls calls for a different investigation from one that develops persistent vibration immediately after an impeller replacement.
The most useful starting point is a comparison with the pump’s previous behavior at similar speed, flow, and slurry conditions. Vibration readings become much more informative when paired with suction pressure, discharge pressure, bearing temperature, motor load, and recent maintenance history. Replacing bearings or balancing an impeller before checking these conditions can leave the underlying problem untouched.
Decide whether to stop before collecting more data
A sudden increase in vibration deserves prompt attention, particularly when accompanied by rubbing or grinding sounds, rapidly rising bearing temperature, significant leakage, visible movement at the base, or unstable discharge. Follow the site’s shutdown criteria and the equipment manufacturer’s limits. If there are signs of mechanical contact or structural movement, continued operation can turn a repairable fault into shaft, casing, or foundation damage.
There is no single vibration limit that suits every slurry pump. Pump configuration, speed, support stiffness, measurement location, and the type of reading all affect interpretation. A velocity reading on a bearing housing cannot be compared directly with an acceleration reading or shaft displacement. Use the applicable equipment limits and a consistent measurement method, supported by historical trends.
If operation remains within approved limits, gather data from designated measurement points without approaching exposed rotating parts. Opening the casing, checking coupling alignment, clearing blockages, or inspecting fasteners requires shutdown and isolation. Lock out the driver and other energy sources, isolate connected process lines, and relieve pressure before opening equipment. Account for slurry temperature, hazardous contents, and solids that may remain trapped inside.
Establish what changed and where the vibration is strongest
Start with the timing. Vibration appearing after maintenance directs attention toward assembly, alignment, clearances, and replacement components. A gradual increase makes wear, deposits, looseness, or bearing deterioration more plausible. An intermittent problem that follows tank level or feed changes suggests a hydraulic disturbance, although more than one fault may be present.
Before changing operating settings, record a compact set of observations:
- Pump speed, flow if available, suction and discharge pressure, and motor current or power.
- Sump or tank level, slurry density, and any recent change in solids concentration or particle size.
- Vibration at the pump and motor bearing housings, using consistent horizontal, vertical, and axial measurement points.
- Bearing temperature, abnormal noise, leakage, and whether readings are steady or fluctuate.
- Recent work on the impeller, bearings, coupling, belts, piping, base, or drive settings.
Keep sensor position, mounting method, and instrument settings consistent. Measurements on thin guards or unsupported covers may reflect local flexing rather than bearing housing motion. Overall readings help establish severity and trends; a vibration spectrum, waveform, and phase measurements can help distinguish possible causes.
Frequency patterns provide clues, but they do not establish a diagnosis alone. A strong component at running speed can indicate imbalance, yet looseness, shaft distortion, and resonance can produce similar behavior. Axial vibration may support an alignment investigation, while high-frequency activity may warrant a bearing assessment. Check that the proposed cause also fits the operating conditions and physical inspection.
Check the hydraulic conditions before dismantling the pump
Slurry pumps can vibrate because the material reaching the impeller is inconsistent or because the operating point has moved outside the intended range. Check tank level, valve positions, suction restrictions, and speed against the normal operating condition. A partially obstructed inlet, settled solids, or a changed discharge system can disturb a pump that is mechanically sound.
Separate cavitation from air entering the suction
Cavitation can produce crackling noise, unstable performance, and irregular vibration. It occurs when local liquid pressure falls sufficiently for vapor cavities to form and subsequently collapse. Investigate low suction level, excessive suction losses, increased liquid temperature, blocked strainers where fitted, and increased pump speed.
Evaluate available suction head using the actual installation and fluid conditions, then compare it with the manufacturer’s requirements and recommended margin. Slurry properties can affect suction losses and pump behavior, so a clean-water calculation may need adjustment or specialist review. Pressure readings must also be interpreted with fluid density, gauge elevation, and pressure reference in mind.
Air entrainment can cause similar symptoms. Look for vortices at the sump surface, inadequate inlet submergence, turbulent feed entering near the suction, and suction-side joints that can admit air. Under suction vacuum, a joint may draw air inward without showing an external liquid leak. Gas released from the process can also affect performance.
If vibration decreases when suction level is restored within the approved operating range, that supports a suction-related diagnosis. It does not prove whether the cause was cavitation, air entry, or another inlet disturbance. Confirm the mechanism before changing the suction arrangement or prescribing a permanent remedy.
Check flow against the pump’s intended operating range
Low-flow operation can create internal recirculation and fluctuating hydraulic forces. Excessive flow can increase suction demand and produce unfavorable loading. Review the pump curve and the permitted operating range for the installed impeller and speed, with appropriate consideration of slurry properties.
Pressure alone does not establish flow. A high discharge pressure may reflect a restriction downstream, while low pressure could result from wear, air ingestion, or excessive flow. Use a reliable flow measurement where available, or a validated assessment of the system.
Avoid attempting to cure vibration by casually throttling the suction valve. This increases suction losses and can worsen cavitation. Any trial involving speed or discharge control should stay within the pump’s operating limits and account for the slurry’s transport requirements. Reducing flow too far can allow solids to settle in piping.
Inspect the impeller and wet end for uneven wear or blockage
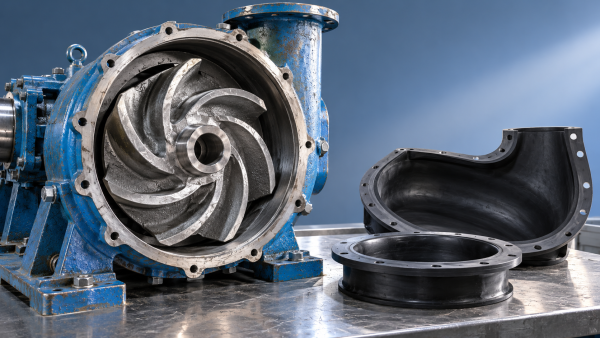
When vibration persists under stable hydraulic conditions, inspect the wet end during a planned, isolated shutdown. Slurry abrasion can remove material unevenly, shifting the impeller’s mass distribution and changing hydraulic forces. Deposits or lodged material can produce a similar imbalance even when the impeller itself remains serviceable.
Inspect the impeller for uneven vane wear, missing material, cracks, trapped debris, and deposits. Check liners and other wear components for distortion, movement, or localized damage. Compare clearances with the manufacturer’s specifications; excessive clearance can impair performance, while insufficient clearance can cause rubbing.
Localized polished surfaces or scoring may indicate contact caused by incorrect assembly, shaft movement, bearing problems, or unsuitable clearances. Replacing the damaged wear part without identifying why contact occurred risks an early repeat failure.
After an impeller replacement, verify the component specification, fit, seating, attachment, and required adjustments. Any balancing work should follow the manufacturer’s procedure. Field grinding to reduce vibration can compromise component geometry or strength.
Check shaft runout where the design permits, using the specified method. A bent shaft or distorted fit can resemble impeller imbalance in vibration data. If uneven wear repeatedly returns, review feed consistency and operating conditions alongside the repair: recurring damage may indicate that the pump duty has changed.
Check alignment, bearings, and the supporting structure together
A slurry pump transfers loads through the shaft, bearings, base, and foundation. Problems in one area can amplify vibration elsewhere. Inspecting these elements together helps avoid treating a bearing failure as an isolated component issue.
Alignment and drive condition
For a directly coupled pump, check angular and offset alignment using the specified procedure and tolerances. Inspect the coupling for worn elements, loose attachments, and assembly errors. Consider whether alignment changes between the cold condition and operating temperature.
For a belt-driven pump, check sheave alignment, belt condition, and tension against the drive specifications. Excessive tension increases bearing loading; insufficient tension or damaged belts can introduce fluctuating forces.
Check for soft foot before final alignment. A machine foot that does not seat correctly can distort the frame as hold-down bolts are tightened. Also investigate pipe strain: connected piping should be adequately supported and should not force the pump into position. A carefully aligned coupling can move out of alignment when piping imposes load on the casing.
Bearings and lubrication
Assess bearing condition using vibration trends, temperature, noise, and lubricant condition together. High-frequency vibration can indicate bearing distress, but hydraulic noise and lubrication problems may complicate interpretation. Bearing fault analysis requires the correct bearing geometry and operating speed.
Check lubricant type, quantity, contamination, and delivery. Adding grease without establishing the lubrication requirement can increase heating through overfilling. Water or slurry contamination calls for investigation of sealing and ingress paths, alongside any bearing replacement.
Where bearing wear or incorrect assembly allows excessive shaft movement, the resulting symptoms may include rubbing, changing clearances, and unstable alignment. Verify axial and radial movement against the equipment specifications.
Base, fasteners, and resonance
Inspect hold-down bolts, bearing housing attachments, the baseplate, grout, and foundation for looseness, cracks, or deteriorated support. Repairing loose connections can reduce vibration, but unexplained recurring loosening should prompt further investigation of the forces acting on the assembly.
Resonance becomes a possibility when vibration rises sharply within a narrow speed range. A controlled speed assessment may help identify this behavior if the process and equipment permit it. Have a vibration specialist evaluate suspected resonance before changing structural stiffness or selecting a permanent speed restriction. The pump must still meet its hydraulic and solids-handling requirements.
Verify the repair under representative slurry conditions
Choose corrective action that addresses both the observed fault and its cause. Repeated impeller imbalance may require attention to uneven abrasion or deposits. Repeated bearing damage may lead back to contamination, alignment, belt loading, or pipe strain. Vibration linked to falling sump level requires a reliable suction condition.
Where practical, make controlled changes so their effects can be distinguished. After repair, confirm assembly, clearances, lubrication, alignment, and guarding before restart. Follow the prescribed startup procedure and monitor vibration, temperature, pressure, motor load, and leakage as operation stabilizes.
Compare the new readings with the original baseline at similar speed, flow, and slurry conditions. A smooth run on water during commissioning may not demonstrate satisfactory behavior with the production slurry. Include the normal operating variations that previously triggered the problem, within approved limits.
Document the confirmed fault, the correction, and the post-repair readings. If vibration remains elevated, revisit the hydraulic and structural evidence before replacing another component. A successful repair should explain why the vibration occurred and show that the pump remains stable through the operating conditions it is expected to handle.
Related Information
 Oct 24, 2026
How Much Should a Froth Pump Be Oversized for Flotation Concentrate?
How much should a froth pump be oversized for flotation concentrate? Learn how inlet air, peak flow, and head affect sizing to avoid costly mistakes and select the right pump.- Oct 24, 2026
Is Higher Hardness Always Better for High-Chrome Pump Castings?
Is higher hardness always better for high chrome pump castings? Discover how toughness, carbide structure, and slurry conditions affect service life—and choose smarter to reduce downtime. - Oct 23, 2026
Which Leakage Test Should You Specify for a Zero-Leakage Knife Gate Valve?
Which leakage test should I specify when ordering a zero-leakage knife gate valve? Compare API 598 and ISO 5208, define seat leakage limits, and avoid costly purchasing mistakes. - Oct 23, 2026
Which Pump Material Lasts Longest in Limestone-Gypsum FGD Slurry?
Which pump material lasts longer in limestone-gypsum desulfurization slurry? Compare high-chrome iron, rubber and duplex steel to find the right fit, reduce downtime and extend service life.

{item.title}
Get a Quote
Please leave your information and email address, and we will contact you as soon as possible.