How Do You Correctly Adjust Impeller Clearance on a Worn Slurry Pump?
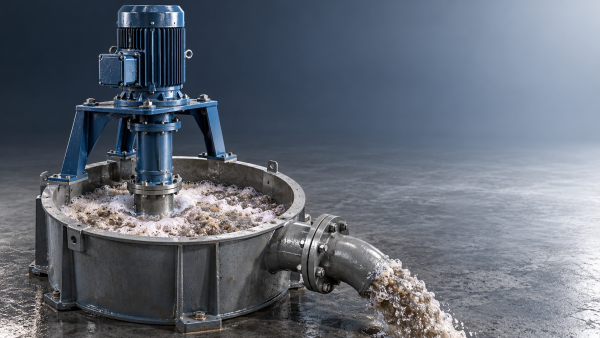
Correctly adjusting impeller clearance on a worn slurry pump starts with identifying the clearance that the pump is designed to adjust, inspecting the worn surfaces, and applying the manufacturer’s setting procedure. Move the specified component in controlled increments, secure the adjustment, and verify free rotation before restarting. Closing a gap without these checks can bring damaged or uneven surfaces into contact while leaving the underlying performance problem unresolved.
There is no universal clearance value for slurry pumps. The correct setting depends on the wet-end design, impeller and liner materials, adjustment mechanism, and specified cold assembly condition. Use the manual for the exact pump configuration, including any replacement impeller or liner fitted during previous repairs.
Identify which clearance the adjustment actually changes
“Impeller clearance” can refer to several different gaps. Many slurry pumps allow adjustment of the axial gap between the impeller’s front face and the suction-side liner or throatbush. Others use an adjustable front liner, shims, or a different arrangement. A closed impeller with a wear-ring arrangement requires a different assessment from an open or semi-open impeller whose vane tips run close to a liner.
Establish which component moves and which surfaces define the specified gap. On a pump with an axially adjustable bearing assembly, moving the shaft changes the impeller’s position relative to stationary wet-end components. That movement can also affect rear clearance, seal geometry, and coupling position. Moving an adjustable suction liner changes a different set of relationships.
An axial adjustment cannot restore a worn radial clearance. If a cylindrical wear-ring interface has enlarged through erosion, moving the impeller along the shaft does not rebuild the missing material. Likewise, adjustment cannot restore vane profiles or impeller diameter lost to abrasion.
Before loosening anything, locate the specified clearance, adjustment direction, locking sequence, tightening torques, and measurement method. If these are unavailable, obtain the correct service instructions before setting the gap. A value taken from a similar-looking pump is insufficient, especially where metal and elastomer-lined variants use different procedures.
Isolate the pump and expose the condition of the wet end
Stop the pump through the normal shutdown sequence, then isolate and lock out its drive and other energy sources. Isolate the suction and discharge connections as required by the installation. Account for static head, trapped pressure, automatic valve movement, and any possibility of reverse flow rotating the shaft.
Drain, depressurize, and flush the casing through the designated connections. Settled solids can remain behind an apparently clear drain, so verify the condition before opening an inspection point or removing a casing section. Handle residual slurry according to its temperature and chemical properties. Support heavy liners and casing components before releasing their fasteners.
Record the existing adjustment position and any accessible clearance before moving the assembly. Also preserve useful operating observations: flow, pressure, speed, motor load, vibration, and recent changes in slurry concentration. These provide a reference when deciding whether the adjustment corrected the original problem.
Clean the clearance surfaces sufficiently to distinguish wear from deposits. Packed solids, scale, or hardened slurry can create a false contact point during adjustment. Inspect the impeller face, vane edges, throatbush, front liner, and relevant rear surfaces for grooves, cracks, missing material, distortion, and rubbing marks.
Decide whether adjustment is still a valid repair
Adjustment is appropriate when the relevant surfaces remain serviceable and the mechanism has enough travel to restore the specified relationship. A broad, reasonably uniform increase in front clearance is different from a deeply grooved throatbush or an impeller with broken edges. Bringing damaged surfaces closer together leaves the erosion channels and weakened features in place.
Evaluate the wear pattern around the circumference. A single polished sector, local contact marks, or a gap that changes markedly as the shaft rotates calls for investigation of runout, bearing condition, seating, or alignment. Moving the impeller toward the closest point can produce rubbing there while leaving excessive clearance elsewhere.
- Uniform recession of otherwise sound mating surfaces: adjustment is a reasonable next step if the manufacturer’s wear limits and available travel permit it.
- Deep channels across the sealing region preserve leakage paths even after the nominal gap is reduced. Assess the component against its replacement criteria.
- Loose bearings or excessive shaft endplay: repair the locating problem first. The impeller will not hold a reliable operating position if the shaft can move beyond its permitted limits.
- Cracked metal, detached elastomer, or a distorted liner requires component repair or replacement before clearance setting.
Confirm that liners are fully seated and that their retaining hardware is sound. Elastomer components deserve particular attention because swelling, displacement, or trapped material behind a liner changes its working surface. Tightening the clearance against a displaced liner creates a misleading setting.
Inspect the adjuster, threads, sliding supports, and locking hardware. Corrosion or accumulated slurry can prevent smooth movement. Do not compensate for a seized assembly by applying excessive force to the adjusting screw; clean and service the mechanism using the prescribed method.
Measure the gap using the specified reference
Use direct measurement where the design provides suitable access. Feeler gauges are useful only when they reach the actual clearance surfaces without bending, forcing the parts apart, or measuring across an erosion groove. Take readings at the locations required by the manual and rotate the shaft by hand to identify variation through a complete revolution.
A dial indicator is useful for tracking axial movement of a shaft or bearing assembly. Mount it on a stable reference and align its contact with the direction of travel. Movement measured at the housing represents a clearance change only if the shaft, bearings, impeller, and stationary parts retain their specified relationships.
Some pumps use a prescribed contact-and-backoff procedure because the working gap is difficult to measure directly. In that arrangement, the approved surfaces are brought gently to the reference position, then separated by a specified amount. Use this method only where the manufacturer permits it; contact can damage some liner materials or create a false reference on unevenly worn parts.
If adjustment is expressed as screw turns, establish the mechanism’s actual movement per turn. For a direct screw mechanism, travel relates to screw lead, which equals pitch only for a single-start thread. Linkages, backlash, and other arrangements can change the relationship. Use the manual’s conversion or measure displacement directly rather than estimating from the appearance of the thread.
Set the clearance without disturbing the assembly
The following sequence applies to a pump whose manufacturer permits axial adjustment of the bearing assembly. An adjustable throatbush, shim-controlled impeller, or wear-ring arrangement needs its own procedure.
- Release the specified locking points. Loosen the bearing assembly clamps or hold-down fasteners only as directed. Leave the assembly adequately supported. Identify any opposing adjuster nuts so that the mechanism can move without loading a locked connection.
- Establish the reference position. Rotate the shaft by hand in the permitted direction while advancing the assembly slowly toward the specified stationary surface. If a contact reference is authorized, stop at the prescribed indication of light contact. Never use motor power to find this position.
- Back the assembly away by the manufacturer’s stated displacement. Approach the final position from the direction specified in the manual so that backlash does not undermine the setting. Where no approach direction is stated, verify the resulting displacement instead of relying solely on adjuster turns.
- Secure the assembly in the required sequence. Tighten the clamps, locking nuts, and hold-down fasteners to their specified torques. Watch for movement during tightening; an assembly can shift as its supports seat.
- Measure again after locking, then rotate the shaft through a complete revolution. Any localized rubbing or inconsistent resistance requires investigation before the pump is returned to service.
When the front liner is the adjustable component, control its position and orientation using the designated hardware. Follow the specified adjustment pattern so the liner remains square to the shaft. A tilted liner creates a narrow gap on one side and a wide gap on the other, even when an average measurement appears acceptable.
For shim-controlled designs, use the approved shim locations and materials. Preserve seating cleanliness and the required clamping arrangement. Removing shims indiscriminately can alter component support or another clearance that shares the same assembly stack.
Do not apply a generic extra allowance for abrasive particles or temperature. The specified cold setting should reflect the design’s operating requirements. If the slurry, operating temperature, or wet-end material has changed beyond the documented configuration, resolve the appropriate setting with the manufacturer before proceeding.
Verify the rear clearance, seal, and drive alignment
After an axial impeller adjustment, confirm any rear clearance or expeller relationship identified in the service instructions. Restoring front clearance can reduce space elsewhere in the wet end. Free rotation alone does not establish that every required gap is within tolerance.
Review the shaft seal arrangement as well. A mechanical seal can require resetting if shaft movement changes its working position or compression. Packing and gland components need sufficient space and the specified adjustment. For pumps with expeller-assisted sealing, confirm the relevant axial relationship rather than assuming that improved front clearance guarantees correct sealing behavior.
If the bearing assembly has moved relative to the driver, verify coupling spacing and alignment according to the coupling and pump instructions. Inspect guard clearances before refitting the guard. Belt-driven arrangements require the corresponding alignment and tension checks when the adjustment affects pulley position.
Complete these checks after the assembly is locked in its final position. Measurements taken while clamps are loose do not represent the condition in which the pump will operate.
Restart under controlled conditions and interpret the result
Reassemble inspection covers and guards, restore the required lubrication and seal services, and prepare the pump for starting. Follow the installation’s priming and valve-position procedure. A slurry pump intended for flooded or primed operation must not be run dry to test whether the impeller is free.
During startup, observe vibration, sound, seal leakage, bearing temperature trend, and motor load. A new scraping sound, abrupt vibration increase, or unexpected load rise warrants stopping and inspecting the setting. Where rubbing is suspected, isolate the pump again before attempting any correction.
Assess hydraulic performance at comparable conditions. Flow, differential pressure, speed, slurry density, and solids concentration must be considered together. A different slurry concentration or discharge restriction can mask the effect of clearance adjustment. Motor current alone cannot prove success: restored flow can increase absorbed power, while rubbing can also raise the load.
If performance remains poor despite verified clearance, inspect the remaining causes supported by the symptoms, including impeller erosion, suction blockage, air ingress, and incorrect speed or rotation. Repeatedly tightening a gap that is already within specification adds contact risk without resolving those faults.
Record the final setting, measurement method, adjustment position, observed wear, and operating readings. Include how much adjustment travel remains. When little travel is left or erosion channels persist, that record establishes the need for wet-end replacement at the next appropriate maintenance opportunity.
Related Information
 Oct 24, 2026
How Much Should a Froth Pump Be Oversized for Flotation Concentrate?
How much should a froth pump be oversized for flotation concentrate? Learn how inlet air, peak flow, and head affect sizing to avoid costly mistakes and select the right pump.- Oct 24, 2026
Is Higher Hardness Always Better for High-Chrome Pump Castings?
Is higher hardness always better for high chrome pump castings? Discover how toughness, carbide structure, and slurry conditions affect service life—and choose smarter to reduce downtime. - Oct 23, 2026
Which Leakage Test Should You Specify for a Zero-Leakage Knife Gate Valve?
Which leakage test should I specify when ordering a zero-leakage knife gate valve? Compare API 598 and ISO 5208, define seat leakage limits, and avoid costly purchasing mistakes. - Oct 23, 2026
Which Pump Material Lasts Longest in Limestone-Gypsum FGD Slurry?
Which pump material lasts longer in limestone-gypsum desulfurization slurry? Compare high-chrome iron, rubber and duplex steel to find the right fit, reduce downtime and extend service life.

{item.title}
Get a Quote
Please leave your information and email address, and we will contact you as soon as possible.