Knife Gate Valve or Pinch Valve: Which Is Better for Tailings?
Should I choose a knife gate valve or a pinch valve for tailings? The answer depends on more than the initial purchase price. Abrasive particles, solids concentration, operating pressure, and maintenance requirements all affect valve performance and service life. Knife gate valves and pinch valves handle slurry differently, making each suitable for particular tailings applications. This guide compares their design, wear resistance, sealing, and operating costs to help you choose the right valve for your process.
The short answer is that a slurry-duty knife gate valve is often a practical choice for isolating a tailings line where a robust gate mechanism and suitable pressure rating are priorities. A pinch valve can be attractive when a replaceable elastomer sleeve is compatible with the slurry and a relatively unobstructed flow path is important. Neither description is enough to make the purchase decision: the exact valve construction and the conditions during opening and closing matter just as much as the valve type.
The difference starts with what touches the slurry
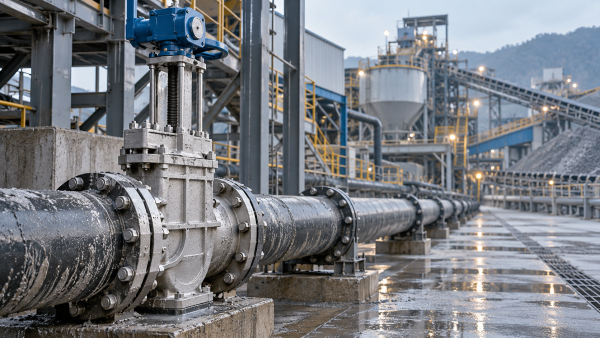
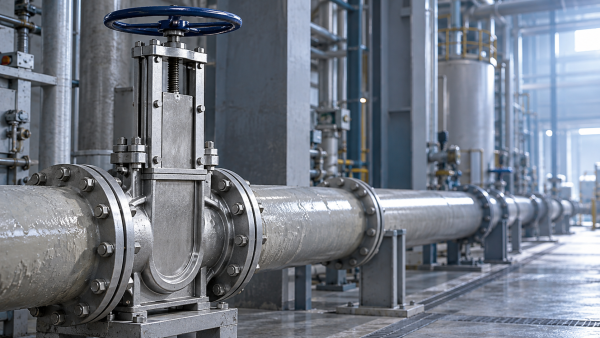
A knife gate valve uses a sliding gate to open or close the flow passage. Slurry designs commonly incorporate elastomer sleeves or seats around the gate, although construction varies. When the valve is open, a suitable full-port design can provide a flow passage close to the pipeline bore. During closure, however, the gate and sealing components must deal with solids in the flow path.
A pinch valve closes by compressing a flexible sleeve. In a properly selected design, the process fluid contacts the sleeve rather than the valve body or closing mechanism. When fully open, the sleeve can provide a relatively smooth, unobstructed passage. The sleeve is also the principal wear and sealing component, so its material and pressure capability are central to the selection.
These are not interchangeable versions of the same valve. A general-purpose knife gate intended for cleaner liquids should not automatically be treated as a tailings valve. Equally, a pinch valve with an unsuitable sleeve can fail prematurely even if its body and connections fit the pipe.
Where abrasive wear occurs
Tailings are not a single material. A fine slurry with a broad particle distribution behaves differently from a stream containing coarse, angular particles. Flow velocity, turbulence, solids settling, and changes in concentration can all affect where wear appears. A valve that performs acceptably in one part of a plant may struggle in another.
Knife gate valves: look beyond the gate
In an open slurry knife gate valve, the bore, sleeves, liners, and any transitions between the valve and adjacent pipework deserve attention. An internal step or misalignment can create a localized wear point. During closure, the gate and seats may be exposed to moving solids, particularly if the valve is operated against flow.
Deposited solids can also obstruct the gate path or prevent the valve from reaching its intended closed position. Some designs manage this better than others through their seat arrangement, flushing provisions, or gate geometry. Ask how the proposed valve handles settled material and whether it can be operated under the actual differential pressure and slurry conditions.
Pinch valves: the sleeve is the wear part
A pinch valve keeps the slurry within its sleeve, but that sleeve must resist abrasion while repeatedly flexing. Material selection involves more than choosing a hard or thick elastomer: resistance to the tailings chemistry, operating temperature, pressure, and expected cycling all matter. A sleeve that resists a particular abrasive stream may not be appropriate for the chemicals or temperature in the same service.
Wear is not necessarily uniform along the sleeve. Upstream bends, pumps, reducers, and partially closed operation can concentrate turbulence. Straight-run recommendations and installation details should therefore be checked against the specific valve manufacturer’s instructions rather than assumed from a generic layout.
Sealing is a design question, not a valve-type promise
Both valve types can be supplied for isolation duty, but neither should be assumed to provide a particular shutoff performance merely because of its name. A pinch valve closes by bringing the sleeve walls together; a slurry knife gate valve seals through its gate and seat or sleeve arrangement. Entrained particles, worn components, differential pressure, and the direction of pressure can affect the result.
For a maintenance isolation point, specify the required leakage performance and the conditions under which it must be demonstrated. Confirm whether the valve must seal in both directions, including when the downstream pipe is drained. Pressure from a static column of tailings can be significant even when pumps are stopped.
Also distinguish process isolation from safe personnel isolation. A single closed valve should not automatically be treated as sufficient protection for intrusive work. The site’s isolation procedure may require additional measures, such as a verified separation or another approved arrangement, depending on the hazard and applicable requirements.
Pressure and actuation can change the choice
Start with the maximum and minimum pressures the valve can see, not just normal operating pressure. Include pump start-up and shutdown conditions, potential pressure transients, static head, and the differential pressure across the closed valve. Check the valve’s rating at the operating temperature and confirm that the seat, sleeve, body, and end connections are all suitable for the specified duty.
Vacuum or sub-atmospheric conditions deserve particular attention with a pinch valve because sleeve behavior depends on the design and any support provided. A valve suitable for positive pressure should not be assumed suitable for vacuum. Knife gate valves also need verification for pressure direction, differential pressure, and any restrictions on operation under unbalanced conditions.
Actuation is another frequent source of late changes. A knife gate actuator must have enough force for the specified pressure and solids conditions throughout the stroke. A pinch valve’s closing arrangement must be compatible with the available operating medium and the pressure needed to close against the process. For pneumatic or hydraulic systems, confirm supply pressure, air quality where relevant, failure position, and the action required after loss of power or control signal.
If a valve must close quickly, ask the process engineer to assess the effect on the pipeline. Closing a moving slurry stream can contribute to pressure transients; the desired response time should be considered alongside the pipeline’s surge analysis, not selected independently.
Isolation or flow control?
Many tailings valves spend most of their lives fully open or fully closed. That is a different duty from holding a partially open position to regulate flow. In a partially closed valve, velocity and turbulence can increase locally, accelerating wear on exposed components.
Some pinch valves are offered for control duties, and certain knife gate designs may also be configured for them. That does not make every isolation valve suitable for throttling. If modulation is required, provide the expected flow range, pressure drop, control frequency, and acceptable wear interval. The supplier should confirm that the particular valve and trim or sleeve are intended for that service.
Intermittent operation can be demanding too. A valve installed on a line that settles during shutdown may need to open through compacted solids or close after slurry has accumulated around the sealing area. Describe the shutdown and restart sequence, including any flushing, instead of specifying only the normal running condition.
Maintenance cost depends on access as much as parts
The purchase price is visible; the cost of a shutdown is often less obvious. Compare the complete maintenance task: depressurizing and draining the line, providing isolation, removing or supporting the valve, replacing worn components, and returning the system to service.
A replaceable pinch sleeve can simplify refurbishment, but replacement may still require the valve to be removed or separated from the line, depending on the design and installation. Sleeve handling, flange access, and the space required to extract the component should be checked before the pipework is finalized.
For a knife gate valve, ask which parts can be replaced in place and which require removal. Gate guides, sleeves, seats, and actuator components may have different inspection and replacement needs. Some slurry knife gate designs also discharge slurry or liquid from the bottom of the valve during operation; where applicable, the installation needs a suitable arrangement to manage that discharge safely.
Spare-parts availability matters more when the tailings line is difficult to bypass. Check sleeve or seat lead times, storage recommendations for elastomers, and whether the actuator or other critical components are interchangeable with equipment already maintained on site. A lower-priced valve is not a saving if its replacement parts cannot be obtained during a planned outage.
Which valve fits the application?
For an isolation point on an abrasive tailings line, a slurry-duty knife gate valve is worth considering when the design meets the pressure, sealing, and operating requirements and the plant can accommodate its maintenance needs. Pay particular attention to solids accumulation, the force required to move the gate, and any discharge generated during cycling.
A pinch valve deserves consideration when keeping the slurry inside a replaceable sleeve is useful and a suitable elastomer is available. It may also be a candidate for flow control if the specific design is rated for that duty. Verify sleeve life expectations, pressure and vacuum limits, and the practical work involved in replacement.
For either option, do not select solely by pipe diameter and nominal pressure. Two valves with matching end connections can have different bore profiles, face-to-face dimensions, actuator loads, and maintenance clearances. Retrofitting an existing line makes these details especially important.
Information to confirm before requesting a recommendation
A useful enquiry gives the valve supplier enough information to assess the complete operating envelope, including abnormal conditions. Gather the following with the process and maintenance teams:
- Pipeline size, material, connection details, flow direction, available installation space, and nearby bends or pumps.
- Solids concentration and how it is expressed, particle size and shape where known, and whether material settles or compacts during shutdown.
- Slurry chemistry and temperature range, including any cleaning or flushing fluids that will contact the valve.
- Normal and maximum pressure, differential pressure in each direction, static head, vacuum exposure, and relevant transient conditions.
- Isolation or control duty, expected cycling frequency, required shutoff performance, and whether operation against flow is necessary.
- Available power or instrument air, required failure position, access for maintenance, and acceptable spare-parts lead time.
Then ask for a recommendation tied to those conditions: the proposed wetted materials, pressure limitations, expected maintenance method, and any assumptions that still need verification. That comparison is more useful than a general claim that one valve type is inherently better for tailings.
Related Information
 Oct 31, 2026
Can a Centrifugal Pump Handle Cement Slurry Without Settling?
Will a centrifugal pump handle my cement slurry without settling? Discover how pump selection, flow velocity and flushing help reduce deposits.- Oct 31, 2026
Knife Gate Valve or Pinch Valve: Which Is Better for Tailings?
Should I choose a knife gate valve or a pinch valve for tailings? Compare wear, sealing, pressure limits and maintenance costs to find the right fit. - Oct 30, 2026
Can a Knife Gate Valve Achieve Zero Leakage in Abrasive Slurry?
Can a knife gate valve maintain zero leakage in abrasive slurry service? Discover the design, testing, and maintenance factors that affect tight shutoff. - Oct 30, 2026
How to Verify High-Chrome Pump Casting Quality Before Shipment
How do I verify the quality of high chrome pump castings before shipment? Discover essential material, hardness, dimensional and traceability checks to ship with confidence.

{item.title}
Get a Quote
Please leave your information and email address, and we will contact you as soon as possible.